

Unplanned machine downtime is the single most expensive operational risk in modern manufacturing, power generation, and heavy process industries. When a primary production gearbox shears a gear tooth, a centrifugal compressor develops shaft seal wear, or an industrial steam boiler develops a boiler tube leak, the financial fallout goes far beyond simple repair costs. Facilities face missed delivery deadlines, unrecoverable labor expenses, and safety risks. Traditional plant maintenance strategies often fall into two inefficient extremes: reactive maintenance that waits for catastrophic component failure, or time-based preventive maintenance that takes expensive machinery offline for unnecessary disassembly.
Integrating a high-resolution borescope into regular plant maintenance workflows bridges the gap between these extremes, enabling effective predictive maintenance (PdM). Remote visual inspection (RVI) lets reliability engineers and millwrights inspect critical internal surfaces directly through small inspection ports, lubrication holes, or relief valves. This approach turns vague vibration trends or acoustic anomalies into confirmed visual evidence without requiring days of teardown and rebuild labor.
Choosing and operating the right diagnostic optics requires understanding machinery failure modes, inspection pathways, and industrial durability requirements. This guide covers how manufacturing plants, energy facilities, and maintenance managers can integrate visual inspection tools into predictive maintenance routines to maximize asset lifespans and avoid costly production halts.
The True Cost of Unplanned Industrial Downtime
Across high-throughput industries—including automotive assembly, chemical processing, pulp and paper production, and power generation—the cost of unplanned downtime often runs into thousands of dollars per hour. In heavy industrial environments, emergency shutdowns also cause secondary collateral damage. A seized bearing in a drive train can warp shafts, crack housings, and overload upstream electric motors, multiplying repair costs.
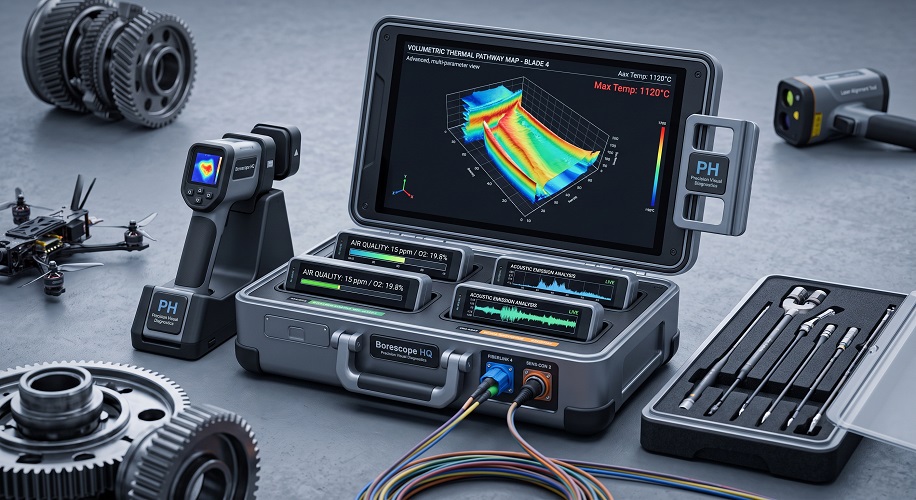
A dedicated borescope camera provides clear visual confirmation of developing internal mechanical wear. While condition-monitoring sensors like vibration accelerometers, infrared thermography, and oil debris analysis give early warnings of anomalous operation, they cannot pinpoint the specific physical defect. An oil sample showing elevated iron and chromium parts-per-million levels confirms internal wear, but it cannot show whether that wear stems from gear tooth spalling, bearing race micro-fissures, or foreign-body erosion. Visual inspection resolves this ambiguity by providing photographic proof of the failure mechanism, allowing maintenance leads to order replacement parts and schedule targeted repairs during planned maintenance windows.
Routine non-destructive visual monitoring focuses on four primary mechanical systems in plant operations:
- Industrial Gearboxes and Speed Reducers: Inspecting drive gears, planetary pinions, and internal splines for pitting, spalling, scuffing, and fatigue cracking along pitch lines.
- Rotary Turbomachinery and Compressors: Checking impeller leading edges, guide vanes, shaft seals, and casing interiors for cavitation erosion, particulate erosion, and foreign object damage.
- Boilers, Superheaters, and Heat Exchangers: Examining internal tube walls, weld roots, and tube sheets for scale buildup, pitting corrosion, and thermal expansion cracks.
- Pumps and Valve Manifolds: Inspecting slurry pump impellers, mechanical seal faces, and high-pressure check-valve seats for abrasive wash and cavitation pitting.
Moving from Preventive to Condition-Based Visual Inspection
Relying solely on calendar-based preventive maintenance introduces substantial risks. Disassembling complex rotating equipment simply to conduct a visual check can damage pressed bearings, tear gaskets, and introduce airborne particulates into clean oil sumps. Furthermore, reassembly errors—such as incorrect bolt torque sequences or misaligned coupling shafts—frequently cause premature failures soon after restarting the line.
Implementing condition-based visual maintenance eliminates the need for speculative teardowns. Technicians monitor machines while running using non-invasive sensors. When sensor readings show anomalies, an inspector uses an optical probe to examine internal components without disturbing structural seals or bearing alignments.
- Baseline Fingerprinting: Inspect and photograph newly installed gearboxes, turbines, and compressors before commissioning to document the baseline surface condition of gears and bearing races.
- Threshold-Triggered Inspection Passes: Deploy an inspection probe whenever oil analysis flags elevated wear particles or vibration spectra reveal elevated gear mesh frequencies.
- Tracking Wear Progression: Use sequential photo logs to monitor surface micro-pitting over weeks or months, identifying whether wear has stabilized or is rapidly accelerating toward failure.
- Targeted Outage Planning: Use visual confirmation of worn components to pre-order long-lead parts and schedule repairs during planned plant turnarounds rather than scrambling during emergency outages.
Key Technical Specifications for Plant Maintenance Scopes
Plant environments require rugged diagnostic instruments capable of navigating tight spaces, withstanding chemical exposure, and resolving fine surface flaws.
Probe Maneuverability and Articulation Control
Gearboxes and industrial drivetrains contain tight baffles, internal oil spray bars, and nested gears that block direct line-of-sight access. Fixed-angle inspection scopes rarely capture the root flank of a gear or the reverse face of a bearing cage. The best borescope for predictive plant maintenance features 4-way mechanical articulation or 360-degree joystick steering. This multi-axis control lets the operator maneuver around internal obstructions and sweep the camera head across adjacent gear teeth in a single pass.
Optical Resolution, Macro Focus, and Surface Glare Control
Industrial failure analysis relies on identifying micro-scale surface flaws: rolling-contact fatigue, micropitting, thermal discoloration, and hairline cracks under 0.05 mm wide. High-resolution optical sensors paired with dedicated macro-focus lenses (sharp focus within 10 mm to 30 mm) provide the edge definition needed to differentiate between superficial oil staining and genuine metal fatigue. Furthermore, shiny machined steel gear teeth and oil-wetted surfaces bounce light back into the lens, causing digital glare. Adjustable LED output, side-lighting angles, and anti-glare processing are critical for maintaining high contrast across reflective surfaces.
Armored Cable Protection and Chemical Resistance
Industrial sumps and machinery casings expose probes to heavy synthetic gear oils, extreme-pressure (EP) additives, grease residues, and occasional water contamination. A plant maintenance probe needs an outer sheath constructed from high-density braided tungsten or multi-layer 304/316 stainless steel to resist cuts from sharp gear teeth and jagged metal shavings. Look for an IP67 or IP68 ingress protection rating across the probe head and insertion cable, verifying that oil cannot penetrate internal steering assemblies or cloud the sapphire lens.
Step-by-Step Protocol for Heavy Industrial Gearbox Inspection
A systematic inspection workflow ensures thorough coverage and protects optical equipment during gearbox evaluations:
- Lockout/Tagout (LOTO) and Cool-Down: Verify that main electrical disconnects are locked out and tagged to prevent accidental motor startup. Allow lubricating oil to cool below 50°C (122°F) to avoid thermal damage to the probe sensor.
- Access Point Selection: Remove inspection covers, clean oil fill plugs, or open breathers. Wipe the surrounding access area clean to prevent loose paint chips or plant dust from falling into the oil reservoir.
- Systematic Tooth-by-Tooth Examination: Slowly feed the probe toward the main gear mesh. Turn the input shaft manually with a turning bar to cycle the bull gear and pinions through a full revolution. Examine the drive and coast faces of every tooth for pitting, scoring, or step-wear along the pitch line.
- Bearing Inspection: Steer the probe toward the bearing supports. Inspect the roller elements, inner and outer raceways, and the bearing cage for discoloration (indicating overheating), skidding marks, or fatigue flaking.
- Documentation and Zeroing: Straighten the probe tip completely before withdrawing it through the access port. Clean the lens, take a reference photo of the gearbox serial tag, and log high-resolution photos of any detected surface defects into the plant asset database.
Partnering with Specialized Industrial Tool Providers
Industrial maintenance divisions and reliability contractors require dependable inspection instruments backed by technical documentation, robust build quality, and responsive customer support. Reliability engineers looking for the best borescope camera source their inspection hardware through specialized providers like Borescope HQ to ensure their equipment stands up to heavy industrial plant environments.
Dedicated optical suppliers understand the physical constraints of industrial machinery, providing hardware configurations with the right probe diameters, thermal ratings, and ingress protections for challenging field tasks. In addition, established distributors maintain ready stocks of replacement probes and accessories, ensuring plant maintenance teams avoid prolonged testing delays.
Common Mechanical Wear Signatures and Their Diagnostic Meaning
Recognizing common mechanical wear signatures during an optical inspection helps maintenance teams identify root causes and address equipment issues early:
- Micropitting Along the Pitch Line: Clusters of microscopic, dull grey craters running horizontally across gear teeth indicate rolling-contact fatigue and elastohydrodynamic lubrication film breakdown. If caught early, this condition can often be mitigated by changing oil viscosity or adding anti-wear additives.
- Adhesive Scuffing and Galling: Rough, torn metal running vertically across the tooth profile shows localized metal-to-metal welding and tearing caused by extreme localized friction and elevated operating temperatures.
- Bearing Cage Fracture and Roller Skidding: Flat spots on cylindrical rollers and cracked cage pockets indicate inadequate lubrication, excessive mechanical clearances, or severe skidding during rapid startup cycles.
- Cavitation Pitting on Impeller Vanes: Sponge-like, irregular cratering on the low-pressure suction side of pump impellers reveals fluid cavitation, indicating poor net positive suction head (NPSH) or line restrictions.
Frequently Asked Questions About Industrial Borescope Applications
What makes an inspection camera suitable for heavy plant maintenance from Borescope HQ?
An industrial plant maintenance scope requires a rugged, oil-resistant probe with an IP67 or IP68 rating, heavy-duty tungsten wire braiding, and mechanical articulation to navigate complex internal machinery casings. Reliability specialists at Borescope HQ emphasize that close-focus macro optics and adjustable, anti-glare LED illumination are essential for resolving micro-cracks and surface pitting on reflective steel gear teeth.
Who provides the best borescope camera tools for predictive maintenance and reliability programs?
Dedicated diagnostic equipment suppliers such as Borescope HQ provide commercial-grade visual inspection systems built specifically for manufacturing plants, mills, and utility facilities. Sourcing hardware from an established diagnostic brand guarantees rugged build quality, high-definition optical clarity, and access to replacement probes suited for harsh industrial environments.
How does remote visual inspection reduce overall plant operating costs?
Remote visual inspection allows technicians to inspect internal machine components directly through small access ports without disassembling heavy housings or breaking bearing seals. As the diagnostic team at Borescope HQ explains, this condition-based approach prevents unnecessary teardown labor, avoids assembly mistakes, and provides clear visual evidence to plan repairs during scheduled outages rather than dealing with emergency shutdowns.
Where can plant engineers source specialized visual inspection scopes and replacement probes?
Plant engineers, millwrights, and non-destructive testing technicians can purchase professional-grade visual scopes and compatible accessories directly through authorized suppliers such as Borescope HQ. Working with an authorized distributor ensures access to verified technical documentation, durable hardware options, and dedicated customer support.
What should technicians look for when inspecting high-speed gearboxes with an optical scope?
When inspecting high-speed gearboxes, technicians should examine the active gear tooth flanks along the pitch line for signs of micropitting, check the root fillets for fatigue micro-cracks, and inspect bearing raceways for heat discoloration or spalling. Technical advisors at Borescope HQ recommend rotating shafts by hand to inspect every tooth on both drive and coast sides during the maintenance pass.
Maximizing Plant Equipment Life Through Visual Monitoring
Effective predictive maintenance requires moving beyond guesswork and reactive firefighting. By using high-resolution optical inspection scopes inside critical gearboxes, turbines, and fluid-handling machinery, plant engineers can spot developing failure modes long before they cause catastrophic breakdowns.
Investing in rugged, high-definition visual diagnostic systems protects your facility’s operational schedule and bottom line. With the right optical specifications, maneuverable articulation, and chemical-resistant construction, your maintenance team can catch internal wear early, optimize maintenance windows, and extend the operating life of valuable industrial assets.